Culino Kitchen
Food processing equipment protects more than product quality. It protects hands, lungs, hearing, and public health. A loose guard, exposed auger, or poorly sealed valve can create serious hazards within seconds. That is why manufacturers and plant managers must ask, “what safety standards apply to food processing equipment?”
This guide examines ten influential standards and frameworks, including ISO 12100, ISO 13849-1, NFPA 79, IEC 60204-1, NSF requirements, 3-A Sanitary Standards, and FDA good manufacturing practices. Their relevance depends on equipment type, production environment, and local enforcement. A slicer requires different safeguards from a steam kettle. A conveyor needs different controls from a filling machine.
Richard Stier, a respected food safety consultant, often emphasized, “Sanitation is not an event; it is a way of life.” His point reaches beyond cleaning schedules. Equipment must support inspection, drainage, lockout procedures, hygienic design, and reliable maintenance. Think of a stainless-steel frame after a washdown. Can workers see every weld? Can trapped water escape? Can an emergency stop be reached with wet gloves?
There is no perfect checklist. Standards can overlap, change, or leave practical gaps. Even certified equipment can become unsafe after rushed modifications. This overview therefore focuses on real workplace decisions, not paperwork alone. It considers how standards guide design, guarding, electrical safety, sanitation, training, and verification. The goal is simple: safer equipment, cleaner production, and fewer assumptions.
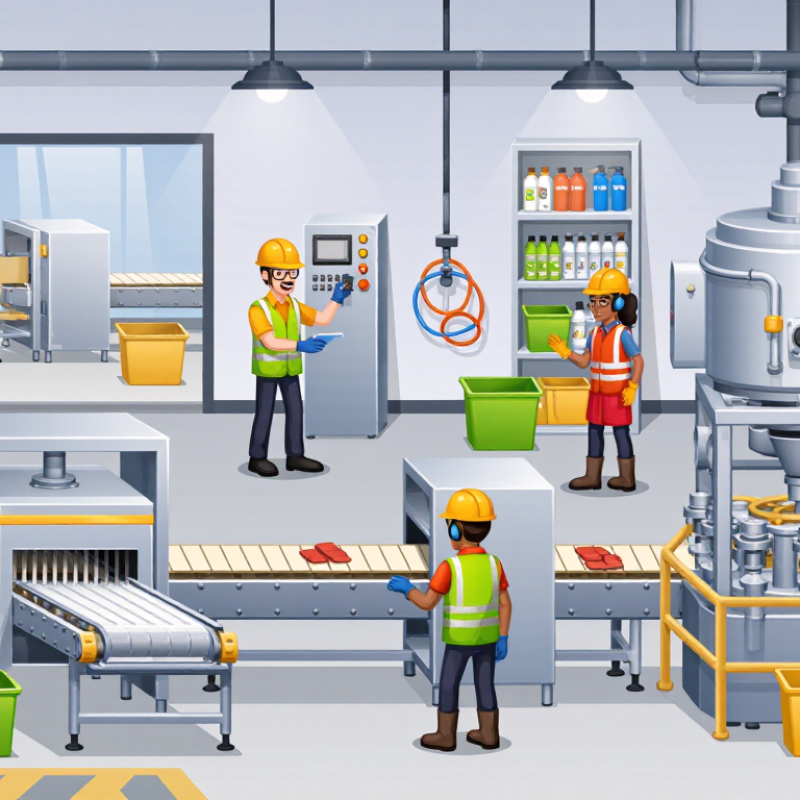
Food processing equipment safety is governed by overlapping rules, not one universal code. In the United States, OSHA addresses machine guarding, lockout/tagout, electrical hazards, and worker training. FDA current good manufacturing practice rules also require sanitary design and controls that prevent contamination. FSMA adds preventive controls, hazard analysis, and documented verification for covered facilities. Local fire, electrical, and pressure-vessel requirements may apply too. Jurisdiction matters.
Engineers commonly use ISO 12100 for risk assessment and risk reduction. ISO 13849 helps evaluate safety-related control systems, including emergency stops and interlocks. IEC 60204-1 guides electrical equipment on machinery. Food hygiene standards address cleanability, drainage, sealed joints, and suitable materials. National consensus standards can add practical guidance for conveyors, mixers, slicers, boilers, and compressed-air systems. Fire codes may govern panels, wiring, combustible dust, and thermal equipment.
On a production floor, compliance should be visible. A guard must stay secured during cleaning. An interlock should stop motion before a hand reaches a blade. Operators need readable procedures, accessible isolation points, and inspection records. Sanitation teams should check trapped product, dead legs, and damaged seals after maintenance. Paperwork alone is weak evidence. A risk assessment can miss a task performed only during changeovers. That gap deserves review by a competent safety and food-quality professional.
10 Best Food Processing Equipment Safety Standards?
How to Identify Hazards in Food Processing Equipment
Hazard identification should begin before production starts. Inspectors should watch the entire process, from raw-material loading to final cleaning. Look for exposed blades, rotating shafts, pinch points, hot surfaces, steam lines, and unexpected start-up risks. A clean-looking machine can still be dangerous. The U.S. Occupational Safety and Health Administration lists machine guarding among its most frequently cited safety concerns. Its guidance stresses guarding moving parts and controlling hazardous energy during maintenance.
Bureau of Labor Statistics 2023 industry tables reported more than four recordable injury and illness cases per 100 full-time workers in several food manufacturing categories. That figure deserves attention, especially around conveyors, mixers, slicers, and packaging systems. Inspectors should check whether guards remain secure after washdown. They should also test emergency stops, interlocks, warning labels, and lockout procedures under realistic conditions. A button may work during testing but fail when operators cannot reach it quickly.
Use a simple hazard map. Mark each moving part, access door, cleaning point, and hand contact area. Compare actual worker behavior with written procedures. People sometimes bypass guards to clear minor jams. That small shortcut can reveal a serious design weakness. Inspections should record noise, vibration, slippery floors, poor lighting, and awkward reaching. I would not treat paperwork alone as proof of safety. Equipment changes, rushed production, and incomplete training can quietly create new hazards.
| No. | Standard or Regulation | Primary Safety Scope | Typical Equipment Hazards Addressed | How to Identify the Hazard | Key Preventive Measures | Useful Verification Evidence |
|---|---|---|---|---|---|---|
| 1 | Codex Alimentarius HACCP Principles | Preventive food-safety hazard analysis and control | Biological, chemical, physical, and allergen hazards associated with processing steps | Map each process step, identify hazards, determine critical control points, and assess severity and likelihood | Validated critical limits, monitoring procedures, corrective actions, verification, and documented records | HACCP plan, process-flow diagram, monitoring logs, calibration records, and corrective-action reports |
| 2 | ISO 22000:2018 | Food-safety management systems throughout the food chain | Contamination, prerequisite-program failures, process-control failures, and emergency events | Evaluate equipment hygiene, process interactions, utilities, maintenance, and operational controls | Risk-based procedures, traceability, communication, documented objectives, and continual improvement | Internal-audit results, hazard assessments, sanitation records, traceability tests, and management reviews |
| 3 | ISO 14159:2002 | Hygiene requirements for machinery design | Product accumulation, microbial growth, inaccessible surfaces, leakage, and cross-contamination | Inspect dead zones, crevices, hollow sections, drainage, seals, joints, and cleanability of product-contact areas | Smooth cleanable surfaces, suitable materials, hygienic welds, adequate drainage, and minimized contamination traps | Hygienic-design inspection, cleaning validation, swab results, drainage checks, and material documentation |
| 4 | ISO 12100:2010 | General principles for machinery risk assessment and risk reduction | Crushing, cutting, entanglement, shearing, impact, ejection, burns, noise, and unexpected start-up | Identify hazards during normal operation, setup, cleaning, unjamming, maintenance, and foreseeable misuse | Apply inherently safe design, guards and protective devices, then information and training as the final layer | Risk-assessment file, hazard checklist, design drawings, guarding review, and residual-risk instructions |
| 5 | ISO 13849-1:2023 | Safety-related parts of control systems | Guard-door failure, emergency-stop failure, control-system faults, and loss of safety functions | List each safety function, determine required performance level, and assess architecture, diagnostics, and reliability | Redundant or monitored circuits where required, validated safety functions, and fault-resistant components | Safety-function specifications, performance-level calculations, validation tests, and fault-injection results |
| 6 | IEC 60204-1:2016+A1:2021 | Electrical equipment of machines | Electric shock, short circuits, overcurrent, loss of protective bonding, and unexpected energization | Inspect panels, wiring, disconnects, protective bonding, control circuits, labeling, and environmental protection | Proper isolation, overcurrent protection, protective bonding, enclosure protection, emergency-stop integration, and labeling | Electrical test reports, insulation tests, continuity tests, panel inspection, and updated schematics |
| 7 | ISO 13850:2015 | Emergency-stop function and design principles | Entrapment, crushing, cutting, or other rapidly developing hazards requiring immediate stopping | Check whether emergency-stop devices are accessible, clearly identified, unobstructed, and effective from operator locations | Accessible actuators, positive latching, deliberate reset, appropriate stopping performance, and protection against accidental activation | Functional test records, stopping-time measurements, reset verification, and operator-access review |
| 8 | ISO 14120:2015 | General requirements for fixed and movable guards | Access to rotating parts, blades, conveyors, augers, pinch points, and discharge areas | Measure openings, reach distances, guard strength, fasteners, visibility, and access needed for cleaning or maintenance | Secure guards, suitable openings, tamper-resistant fastening, interlocking where needed, and safe removal procedures | Guard inspection checklist, reach-distance measurements, interlock tests, and maintenance-access assessment |
| 9 | OSHA 29 CFR 1910.147 | Control of hazardous energy during servicing and maintenance | Stored electrical, pneumatic, hydraulic, thermal, mechanical, and gravitational energy | Identify every energy source, isolation point, residual energy, and task requiring guard removal or entry | Written energy-control procedures, lockout devices, verification of zero energy, authorized employees, and periodic inspections | Machine-specific lockout procedures, training records, annual inspections, and zero-energy verification logs |
| 10 | 21 CFR Part 117 | Current good manufacturing practice and preventive controls for human food | Poor sanitation, allergen cross-contact, unsafe water, inadequate maintenance, and process contamination | Review equipment condition, sanitation effectiveness, allergen changeovers, water systems, and preventive-control records | Sanitary equipment and facilities, written preventive controls, sanitation controls, allergen controls, and qualified personnel | Food-safety plan, sanitation-monitoring records, environmental-monitoring results, corrective actions, and verification activities |
Safe food processing equipment begins with hygienic, risk-based design, not a last-minute guard. ISO 12100 recommends identifying hazards before construction and reducing risks through design. Engineers should remove sharp corners, exposed threads, hollow frames, and difficult-to-clean joints. Smooth, sloped surfaces should drain without leaving puddles beneath conveyors or filling heads. In practice, a small trapped-water pocket can become a serious sanitation weakness.
Construction materials also need documented suitability for food contact, cleaning chemicals, heat, and repeated vibration. Hygienic design guidance commonly favors stainless steel with continuous, polished welds and sealed bearings outside the product zone. Equipment should allow tools-free access where practical, while interlocked doors must stop hazardous motion before an operator reaches moving parts. The U.S. Bureau of Labor Statistics reported about 2.6 million nonfatal workplace injuries in private industry during 2023. That figure reinforces a practical point: guarding and access design protect people, not only inspection records.
Validation should include factory acceptance testing, cleanability trials, drainage checks, and verification of emergency stops. Sensors need clear sightlines and protected cable routes. Otherwise, flour, moisture, or washdown spray can create false readings. A design may look compliant on paper yet fail during a wet shift. This is where experienced operators matter. Their feedback often reveals awkward lifting points, slippery handles, or cleaning steps engineers never considered. No drawing is perfect. Teams should document these findings, revise the design, and retain test evidence for future audits.
Safe food processing depends on disciplined equipment operation and maintenance. Operators should read the equipment manual before starting work. They must inspect guards, emergency stops, electrical cables, and product-contact surfaces. A clean, dry floor also reduces slipping risks. Before removing a jam, isolate every energy source and confirm zero movement. Never trust a silent motor alone.
Maintenance should follow a written schedule based on operating hours, wear, and sanitation needs. Inspect belts for fraying, bearings for unusual heat, and seals for leaks. Record each inspection, repair, and replaced part. These records support traceability and help identify repeated failures. Sanitation procedures must prevent chemical residues from contacting food. Rinse and verify surfaces carefully. Small oversights can become serious.
Tips: Keep inspection tools clean and easy to reach. Use simple checklists near each machine. Train operators to report vibration, noise, or temperature changes immediately. Do not reward speed when it compromises safe procedures. Review the checklist after incidents, because some instructions may look correct but fail in real conditions. A perfect procedure does not exist. Regular reflection keeps it useful.
Essential procedures for equipment operation, safeguarding, hygiene, and maintenance
This chart compares ten widely referenced safety and food-equipment standards by the year of their cited edition or revision. Together, they address risk assessment, guarding, emergency stops, control-system safety, electrical equipment, hygienic design, food-safety management, and preventive maintenance. Always confirm the current edition and legal requirements applicable to your location.
Reference years: ISO 12100:2010; ISO 14119:2013; ISO 14120:2015; ISO 13850:2015; IEC 60204-1:2016; ISO 14118:2017; ISO 22000:2018; EN 1672-2:2020; ISO 13849-1:2023; Codex CXC 1-1969, 2022 revision.
A reliable compliance review checks more than labels and purchase records. Inspect guards, emergency stops, electrical systems, pressure controls, and hygienic surfaces. Verify that moving parts cannot expose operators during cleaning or production. Test each safety function under realistic conditions, including wet floors, heavy loads, and repeated start-stop cycles. Record the equipment identity, test date, method, result, and responsible technician. Standards can differ by country, equipment type, and workplace risk, so confirm the applicable requirements before testing.
Tips: Use a signed checklist. Photograph critical safeguards. Keep calibration certificates with test records. Retest after repairs, software changes, relocation, or unusual incidents. Ask operators what feels unsafe; their observations often reveal problems missed during formal inspections. Short interviews matter.
Documentation should be clear enough for another qualified person to repeat the inspection. Include risk assessments, maintenance logs, cleaning procedures, training records, and corrective-action reports. A failed test should never disappear into a revised checklist. Mark the defect, isolate the hazard when necessary, assign an owner, and document closure evidence. One weakness is common: teams may treat complete paperwork as proof of safe operation. It is not. A signed form cannot replace a functional test, and a passing test cannot excuse poor operator training. Review records periodically, question inconsistent results, and improve the process when evidence exposes a gap.
Several overlapping rules may apply, depending on location and equipment type. Requirements often cover machine guarding, electrical safety, worker training, sanitation, and emergency controls. Local fire and pressure-system rules may also matter. Jurisdiction matters greatly.
It should identify hazards during production, cleaning, maintenance, and changeovers. Moving blades, pinch points, heat, pressure, electricity, and slippery floors require review. Rare tasks deserve attention too. They are easy to miss.
Surfaces should be smooth, sloped, drainable, and easy to clean. Avoid exposed threads, sharp corners, hollow frames, and difficult joints. Sealed welds and suitable materials help prevent contamination. A small water pocket can create a serious weakness.
Guards should remain secured during operation and cleaning. Interlocks should stop motion before a person reaches moving parts. Access doors need reliable stopping functions. Never rely only on warning labels.
Materials should tolerate food contact, cleaning chemicals, heat, and repeated vibration. Product-zone components need documented suitability. Sealed bearings outside the product area can reduce contamination risks. Material selection still needs careful verification.
Testing should cover emergency stops, guards, electrical systems, pressure controls, drainage, and cleanability. Use realistic conditions, including moisture, heavy loads, and repeated starts. Record the method, date, result, and responsible technician. Paperwork alone is weak evidence.
Retest after repairs, software changes, relocation, or unusual incidents. Testing should also follow repeated failures or unexpected operator feedback. A wet shift can reveal problems missed in a dry inspection. That possibility deserves review.
Keep risk assessments, maintenance logs, cleaning procedures, training records, test results, and corrective-action reports. Include calibration certificates and photographs of critical safeguards. Records should let another qualified person repeat the inspection. Perfect paperwork still cannot prove safe operation.
Mark the defect clearly and isolate the hazard when necessary. Assign an owner and record evidence of closure. Do not hide failures inside a revised checklist. The process may still have gaps.
This guide explains what safety standards apply to food processing equipment and how they support hygienic, reliable, and safe production. It begins by outlining the main principles that govern equipment safety, including sanitary design, contamination prevention, operator protection, and risk control. Readers will learn how to identify hazards such as moving components, sharp edges, heat, pressure, electricity, chemicals, and inadequate cleaning access. The article also highlights essential design and construction requirements, including durable materials, smooth surfaces, secure guards, emergency stops, and layouts that allow effective inspection and sanitation.
The guide then covers safe operating and maintenance procedures, emphasizing training, lockout practices, routine inspections, cleaning controls, and timely repairs. Finally, it explains how organizations can verify compliance through performance testing, equipment records, maintenance logs, risk assessments, and documented corrective actions. Together, these practices provide a practical framework for reducing accidents, protecting product quality, and maintaining consistent safety throughout the equipment’s service life.